| Client | A European sports and outdoor brand |
| Sector | Sports & Outdoor |
| Region | Europe |
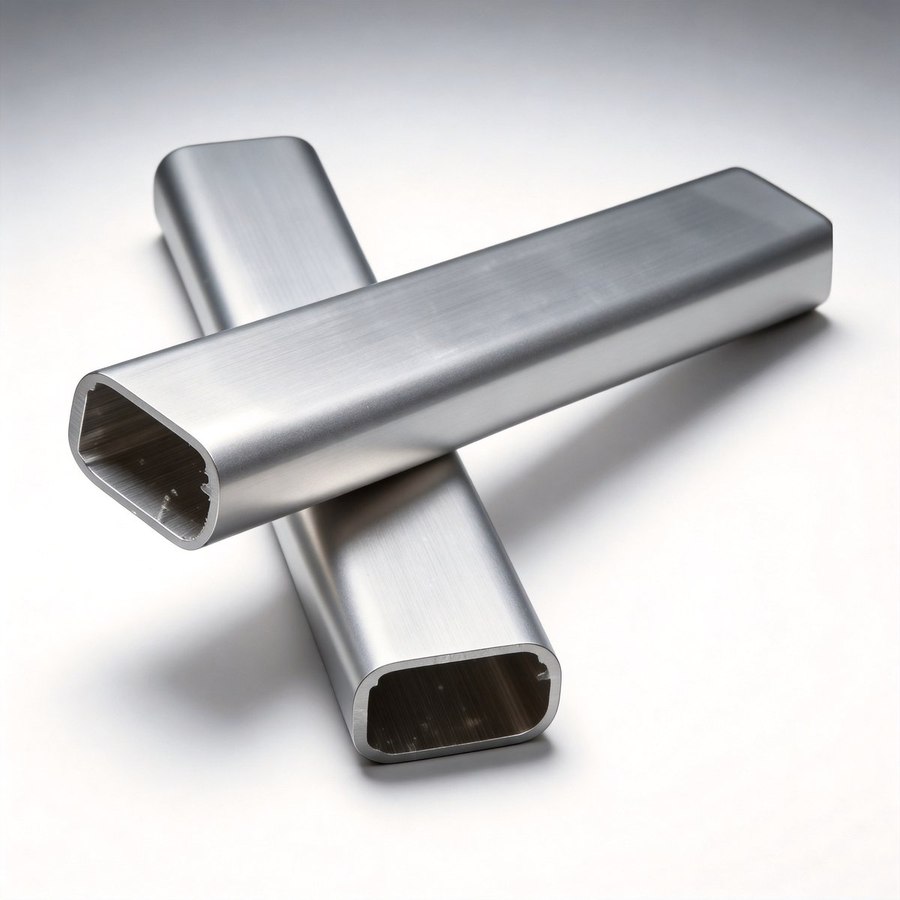
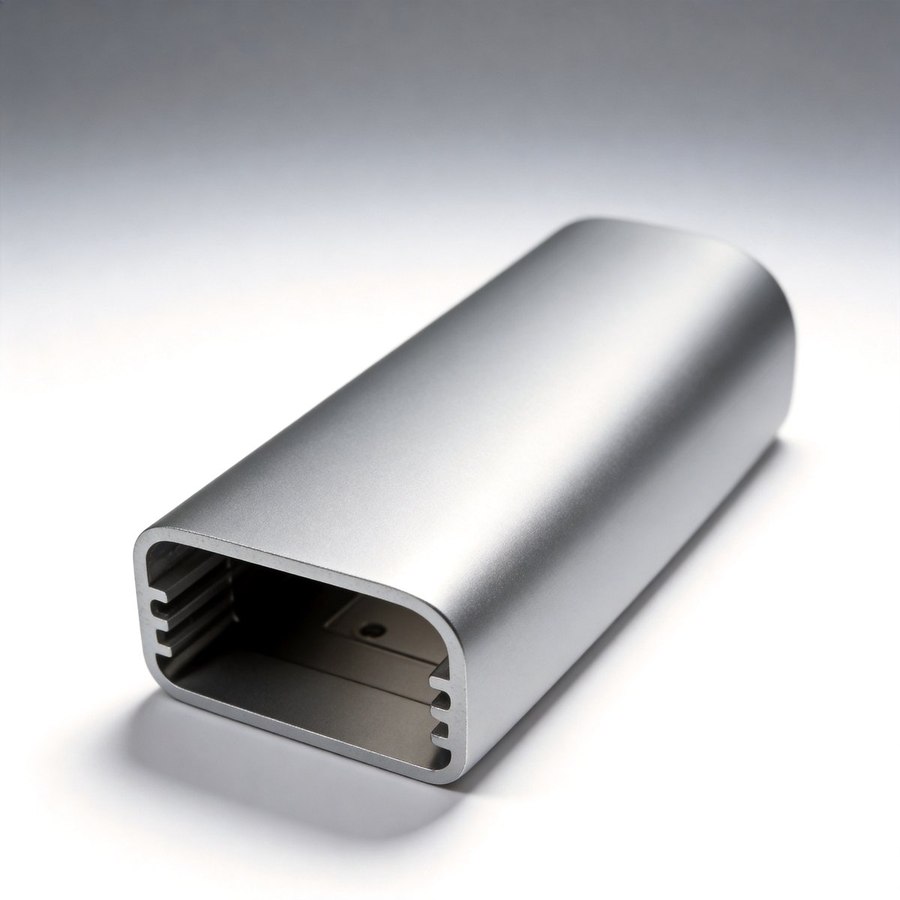
| Programme | Bicycle headlight aluminium profiles |
Client identity is described by market position rather than by name, in line with our confidentiality commitments.
Bicycle headlight aluminium profiles for a European sports brand — from drawing confirmation to first sea-freight delivery in 19 days.
The challenge
The customer had a season to hit. The risk was not whether we could make the profile but whether the whole chain — DFM, tooling, sampling, approval, production and ocean freight — could compress into weeks rather than months. European seasonal product does not get a second launch window.
What we did
DFM and tooling run in parallel with the customer's decision
Our engineers reviewed the cross-section within one working day while the customer was still finalising internal sign-off, so no calendar time was lost between approval and die cutting.
4–5 day tooling, 7 day samples
New die developed in 4–5 days and first samples in 7 days, with three rounds of free sampling included — so if the first article needed a tweak, the schedule was not reset to zero.
Production started within 24 hours of approval
Once samples were signed off, mass production began inside 24 hours rather than entering a queue.
Export packing and documentation prepared in parallel
Pearl-cotton cushioning inside wooden crates, with commercial invoice, packing list and certificate of origin prepared while production ran, so nothing waited on paperwork at the port.
Results
| Result | Measured |
|---|---|
| 19 days | Drawing confirmation to first sea delivery |
| 4–5 days | New die development |
| 24 h | Mass production start after sample approval |
- 19 days from drawing confirmation to first sea-freight delivery.
- Tooling, sampling and production compressed without skipping inspection.
- Export packing and documentation ready in parallel with production.
- Seasonal launch window met.
Why it held in production
Every stage of this programme ran inside our own plant — tooling design, extrusion, CNC machining, surface treatment and assembly. That is the reason the result repeated rather than appearing once on a first article: when a parameter needs adjusting, we change it and verify it the same day instead of negotiating through a subcontractor. We hold ISO 9001 across the process, with wall thickness at ±0.02 mm against a GB standard of ±0.05 mm and cut-to-length at ±0.005 mm.
Other programmes
Have a similar enclosure programme? Send your drawing and we will review it free of charge.