| Client | A major atomiser manufacturer |
| Sector | Atomisation Technology |
| Region | China, supplying regulated export markets |
| Programme | Atomiser housings to high-cleanliness specifications |
Client identity is described by market position rather than by name, in line with our confidentiality commitments.
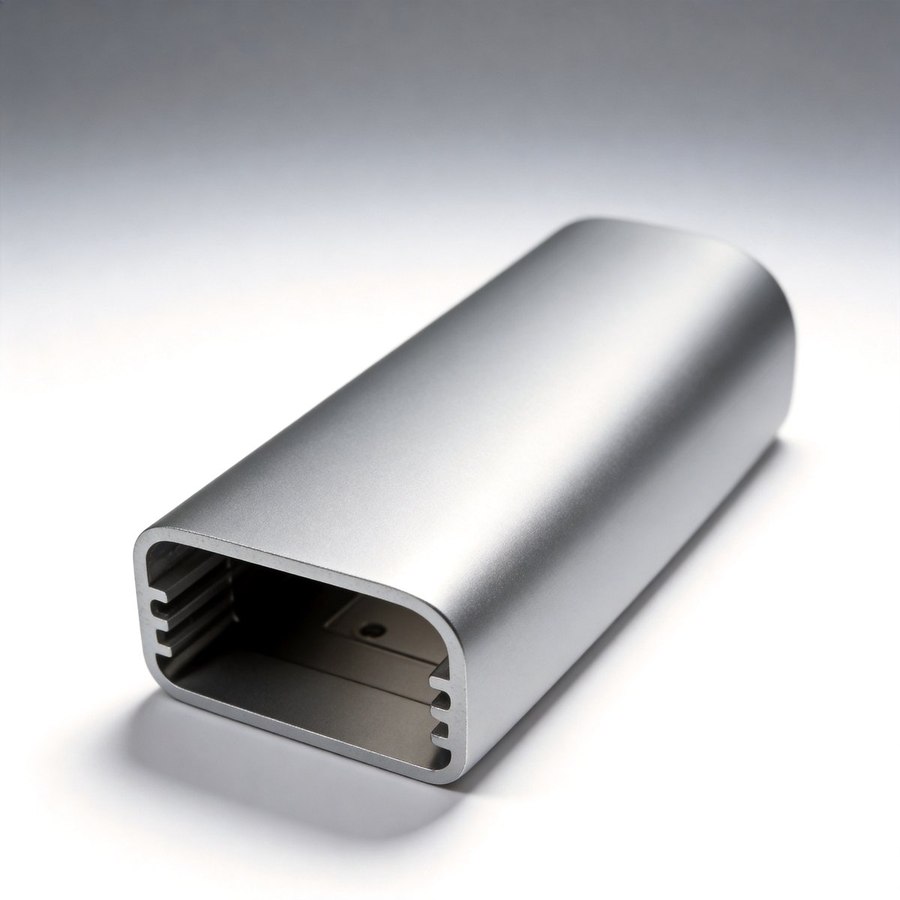
Atomiser housing profiles produced to high-cleanliness handling requirements, where surface condition and residue control matter as much as dimensional accuracy.
The challenge
High-cleanliness work changes what the process has to control. Dimensional accuracy is table stakes; the additional requirement is surface condition — no embedded contamination, controlled handling, and finishing that does not leave residue in the section. This has to be designed into the process route before the first article, not inspected in afterwards.
What we did
Cleanliness handled as a process route, not a final check
Handling, packing and surface expectations were agreed at enquiry stage so the route was set before production rather than negotiated after the first article.
Uniform substrate reduces downstream remediation
A billet route with ceramic filtration, degassing and homogenising produces a clean, uniform surface, so there is less to correct later — and less correction means fewer handling steps that could reintroduce contamination.
Machining and finishing in one plant
Because CNC machining, surface treatment and packing all happen under our own roof, cleanliness requirements do not have to be re-specified at each transfer between suppliers.
Dimensional control maintained alongside cleanliness
Inner and outer diameters held to ±0.04 mm and walls to ±0.02 mm, so meeting the cleanliness requirement did not come at the cost of fit accuracy.
Results
| Result | Measured |
|---|---|
| ±0.04 mm | Inner / outer diameter tolerance maintained |
| 1 | Plant handling every stage of the route |
| 100% | In-house, no subcontracted finishing |
- Atomiser housings supplied to the customer's high-cleanliness requirements.
- Process route agreed before first article rather than retrofitted.
- Cleanliness and dimensional accuracy held simultaneously.
- All stages handled in one plant, with no third-party transfers.
Why it held in production
Every stage of this programme ran inside our own plant — tooling design, extrusion, CNC machining, surface treatment and assembly. That is the reason the result repeated rather than appearing once on a first article: when a parameter needs adjusting, we change it and verify it the same day instead of negotiating through a subcontractor. We hold ISO 9001 across the process, with wall thickness at ±0.02 mm against a GB standard of ±0.05 mm and cut-to-length at ±0.005 mm.
Other programmes
Have a similar enclosure programme? Send your drawing and we will review it free of charge.