| Client | A global audio equipment brand |
| Sector | Audio & Digital Accessories |
| Region | Global |
| Programme | Docking station shell structural optimisation |
Client identity is described by market position rather than by name, in line with our confidentiality commitments.
Structural optimisation of a docking station shell that raised bending strength by 18% at 0.8 mm wall thickness — without adding material or weight.
The challenge
The customer wanted a thinner section but could not give up stiffness: at 0.8 mm the shell was flexing more than the product could tolerate. The obvious answers — thicken the wall or change alloy — both cost weight and money, and neither was acceptable to the industrial design team.
What we did
Stiffness put into the geometry, not the wall
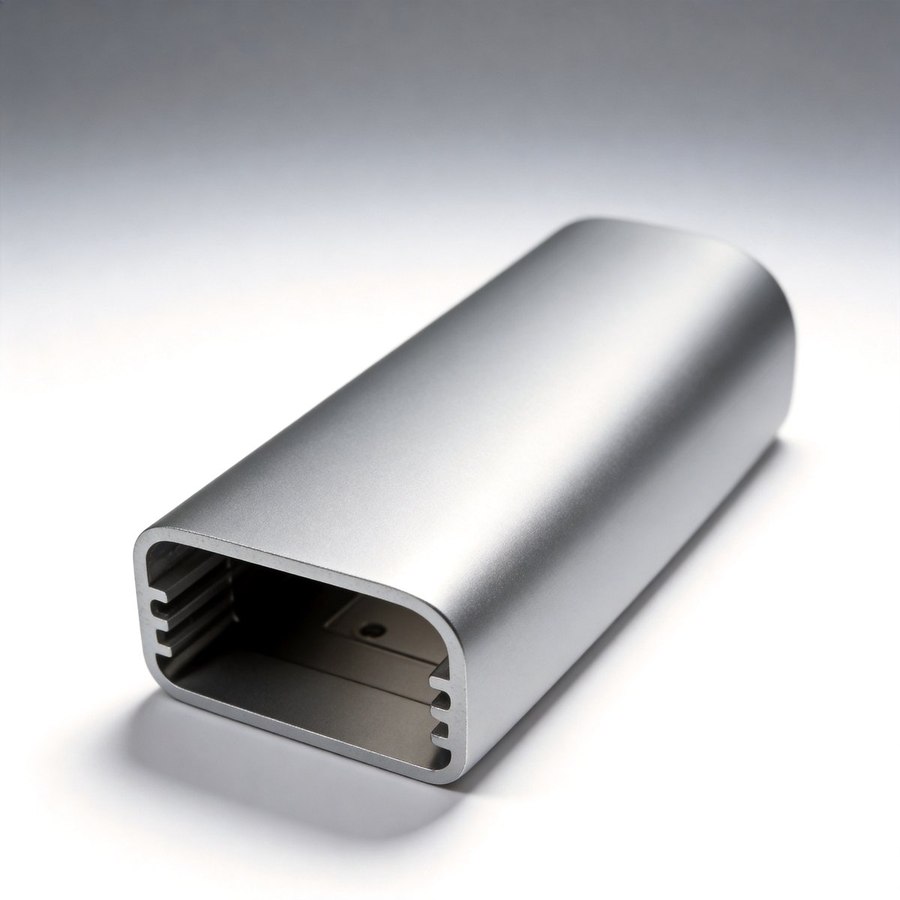
Rather than thickening the section, we reworked the internal ribbing and chamber layout so the section itself carried more load. Ribs and chambers are extruded features, so this added no material and no machining time.
Wall uniformity held so the thin section behaves predictably
Wall thickness controlled to ±0.02 mm against a GB standard of ±0.05 mm. A thin wall only performs as designed if it is actually the thickness you specified across the whole length.
Free DFM review as the starting point
The improvement came out of the design review rather than out of a tooling change: our engineers flagged the flex risk and proposed the geometry change before any die was cut, so it cost nothing to implement.
Validated through sampling, not assumption
Three rounds of free sampling let the revised section be physically validated before volume production, so the improvement was confirmed rather than modelled.
Results
| Result | Measured |
|---|---|
| +18% | Bending strength at the same wall thickness |
| 0.8 mm | Wall thickness maintained |
| 0 | Added material or weight |
- 18% higher bending strength at 0.8 mm wall thickness.
- No additional material or weight added to the section.
- Improvement identified during free DFM review, before tooling was committed.
- Validated through physical sampling rounds before volume production.
Why it held in production
Every stage of this programme ran inside our own plant — tooling design, extrusion, CNC machining, surface treatment and assembly. That is the reason the result repeated rather than appearing once on a first article: when a parameter needs adjusting, we change it and verify it the same day instead of negotiating through a subcontractor. We hold ISO 9001 across the process, with wall thickness at ±0.02 mm against a GB standard of ±0.05 mm and cut-to-length at ±0.005 mm.
Other programmes
Have a similar enclosure programme? Send your drawing and we will review it free of charge.